FP as a length stop
The program moves the stop to the selected measure. The operator brings the workpiece to the reference and carries out the agreed cutting cycle.

OMGA / NC POSITIONERS FP FOR SAWS
The OMGA FP NC positioner sets the length reference or, with suitable equipment, feeds the material. Learn the difference between a stop and a pusher and the conditions for connection to the saw.
Explore the options ↓ Official page ↗
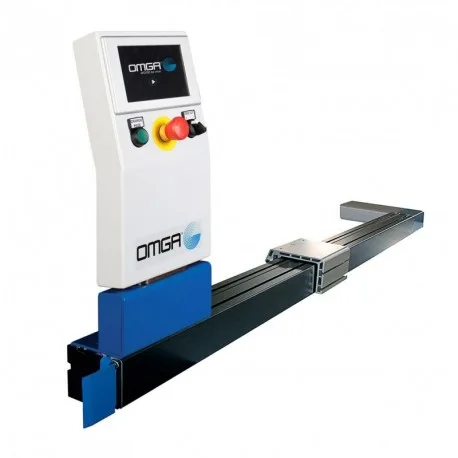
TWO WAYS OF USE
The program moves the stop to the selected measure. The operator brings the workpiece to the reference and carries out the agreed cutting cycle.
A moving unit with suitable grip or support moves the material. Automatic sequence requires a suitable saw, control connection and safety equipment.
WHO MOVES WHAT?
You select the length. The positioner moves the reference stop; the workpiece therefore does not move yet.
The program moves the stop.You bring the workpiece to the prepared reference. Clamping and cutting follow the saw’s intended procedure.
A person moves and prepares the material.In a suitably equipped combination, the push unit guides the material to the next cut. This is a different working method from the stop alone.
The connected system coordinates positioning and cutting.SELECT DIRECTION AND STROKE
FP is available in left- and right-hand versions. The direction is chosen according to the saw layout and material flow, and the stroke according to the tasks and available space.
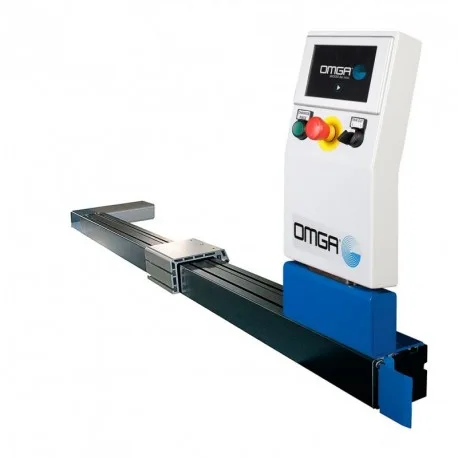
| FP 2000 | 2000 mm |
|---|---|
| FP 3000 | 3000 mm |
| FP 4000 | 4000 mm |
| FP 5000 | 5000 mm |
| FP 6700 | 6700 mm |
The positioner travel is neither the total installation length nor an arbitrary maximum workpiece length. When planning the layout, the saw, support tables, clamping and access must be taken into account.
Technical source: OMGA · FP 6700 - DX ↗
Technical source: OMGA · FP 6700 - SX ↗
CONTROL AND DATA
7-inch touchscreen. The manufacturer describes fence, pusher and frame modes, and storage for up to 500 programs. A function in the program does not yet mean that all the necessary mechanical equipment is included.
CSV support for importing lists, operation in millimetres or inches and communication ports. We agree the format of your list and the transfer path with the selected control system.
A dedicated mode helps prepare frame dimensions. The presented V-joint and 45° corner-saw connections require suitable stops, reference calculation and configuration.
The brochure lists USB, two RS232 and RJ45. Connectivity enables the agreed data flow; it does not guarantee automatic compatibility with every business or design program.
| Maximum feed speed | 60 m/min |
|---|---|
| Stated positioning accuracy | ±0,1 mm |
| Programs | up to 500 |
| Layout | left or right |
Positioning accuracy is not a guaranteed tolerance of the final cut piece. Reference, saw, clamping, material and setting also affect it. We verify the required tolerance on the complete combination.
BASIC PACKAGE AND OPTIONS
Roller or sliding tables, supports, the position of the fence, space for movement and material handling. Long and delicate profiles need an adequately supported travel path.
Connecting kit and the method of signal exchange with the saw. An independent positioner does not turn the basic saw into an automatically safeguarded line.
Optional material clamping, more precise measurement, fence damper and references for 90° or 45°. The choice follows the actual workpiece and cycle.
Optional code reading or label printing can support order organisation. Before integration, we define what data the code contains and where it is transferred.
CATALOGUE AND OFFICIAL VIDEOS
Layouts, modes of use, software functions and optional equipment.
Official PDF · 3 pages · 2.2 MBPRACTICAL QUESTIONS
First we need the saw manufacturer, model and version, a description of the tables and the required method of work. We check the mechanical, control and safety connection; we do not promise universal compatibility.
FP positions the material; it does not perform the cut. Suitability for wood, plastic or metal profiles is determined by the machine, clamping and the complete setup.
Stored lengths reduce repeated setting changes. However, the correct initial reference, setting checks and result verification remain part of the job.
EQUIPMENT SELECTION
Specify the material, cross-section, input and final lengths, angles and approximate quantity. Add a description of the current working method. This allows us to determine the right saw, clamping, feed and software options.
Send enquiry ↗The form keeps the source page. The version, accessories and price are determined in an individual offer.